
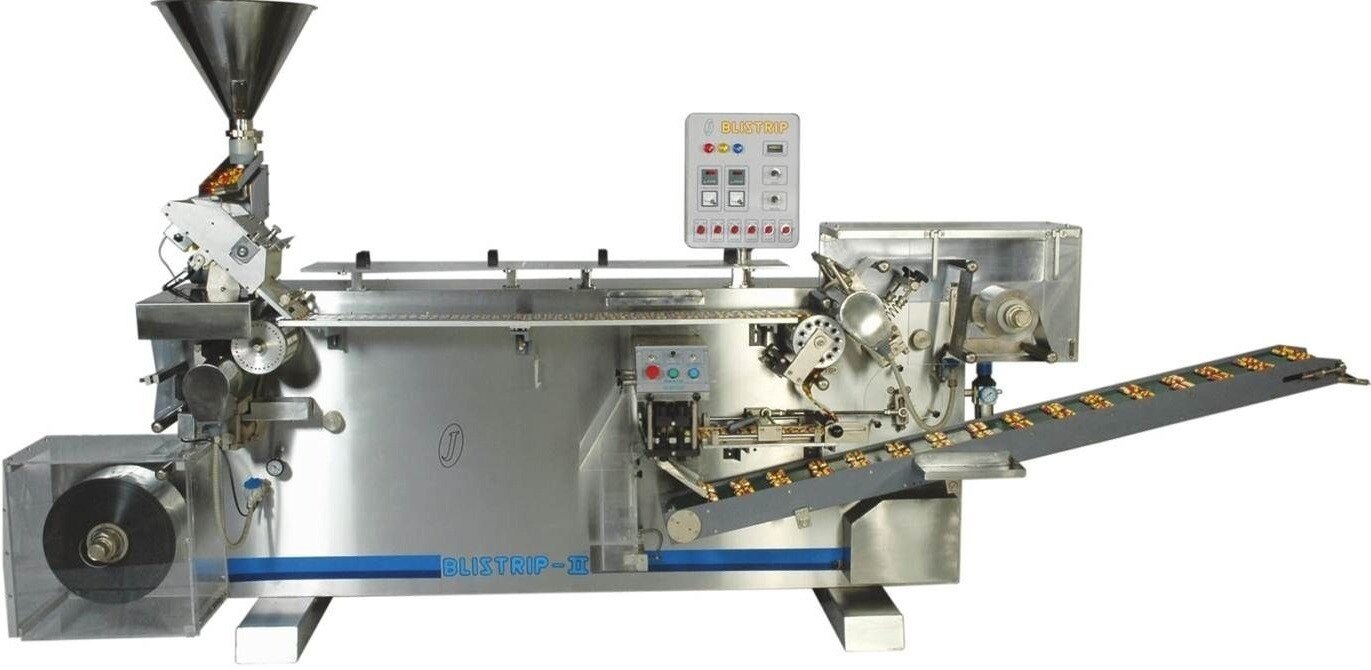
Recovering tablets or capsules from rejected blister cards is not simply a matter of opening the pack faster. By the end, you will know how to assess separation performance, match equipment to blister construction, approve new formats, control contamination, and decide when mechanised recovery is justified.
Key takeaways
- Measure recovery rate, product damage and line speed together.
- Match punch geometry to tablet shape, capsule size and blister material.
- Approve recovered product only after documented quality and identity checks.
- Compare recovery value with labour, cleaning time and rejected-product risk.
What a De-Blistering Machine Does and How to Measure Its Performance
A de blistering machine separates usable tablets or capsules from rejected blister cards without treating the pack as waste. The operator loads cards into a feed system, which indexes each cavity beneath a punch, roller or stripping tool.
Controlled force breaks or peels the lidding material, releases the dose through a discharge chute, and sends empty foil-plastic shells to a separate bin. Adjustable force matters: too much chips coatings or splits capsules; too little leaves product trapped.
A typical operating sequence is:
- Load cards in the specified orientation and align pockets with the tooling.
- Apply the selected punch or roller pressure to open each cavity.
- Collect released doses in a controlled, labelled container.
- Discharge empty cards separately for inspection and reconciliation.
- Record stoppages, changeovers and cleaning time.
This is different from cutting cards or pushing doses through foil by hand. A tablet deduster removes loose dust; it does not open sealed pockets or separate empty packaging.
Measure the machine with an acceptance profile, not packs per minute alone.
| Figure | What it measures | Failure it exposes |
|---|---|---|
| Recovery yield | Usable doses recovered ÷ doses fed | Product left in pockets |
| Intact-dose rate | Undamaged doses ÷ recovered doses | Chipping, cracks or capsule splits |
| Reject rate | Unusable doses and empty pockets | Poor separation or feeding |
| Residual contamination | Foil or plastic found with doses | Inadequate stripping or discharge |
| Downtime | Minutes lost to jams, cleaning and changeover | Hidden production loss |
A pharmaceutical machines manufacturer should provide these records across the actual blister materials, sizes and speeds you will run. Vision inspection finds missing or visibly damaged doses, but laboratory testing remains necessary for coating integrity, dose uniformity and chemical quality.
How Blister Materials, Product Shapes and Machine Geometry Affect Recovery
Whether a dose leaves intact depends on the force needed to open its cavity, not simply on machine speed. A setup proven on push-through PVC/aluminium blisters can crack tablets, split capsules or leave foil attached when used on a different construction.
| Construction | Machine implication | Typical failure |
|---|---|---|
| PVC with aluminium lidding | Controlled punch force and support | Crushed edges or incomplete extraction |
| PVdC-coated PVC, PET or ACLAR | Higher barrier-film resistance needs adjusted separation force | Torn film and trapped product |
| Cold-form aluminium | Rigid pockets need stronger support and different tooling | Deformed capsules or tablet abrasion |
| Deep pockets, thick foil or high seal strength | More travel and force are required | Broken doses or residual fragments |
Shape matters just as much. Long caplets, scored tablets, soft capsules and coated tablets contact punches differently; a narrow punch can chip an edge, while excessive pressure can rupture a capsule. Pocket depth and radius must give the product a clean escape path.
Pocket indexing must centre each cavity under the punch or roller. Product guides, pocket supports, feed orientation, discharge chutes and reject settings then need adjustment for that geometry. During changeover, a machine can run smoothly while producing hidden damage.
Qualification should challenge the smallest and largest formats, every relevant lidding material, speed limits and restart conditions. A pharma machinery manufacturer should document these settings for each de blistering machine for care products or pharmaceutical products.
How to Run a Format Trial and Approve Recovered Product
Approve a new setup only after a documented format trial shows that recovery is repeatable and recovered units remain suitable for their intended use. Test production material, not a convenient substitute. A pharmaceutical machinery manufacturer should provide format-specific setup instructions and acceptance criteria before the run begins.
1. Record the product, batch, tablet or capsule dimensions, blister material, pocket dimensions, lidding material, tooling identification, feed settings, punch or roller force, machine speed, and reject settings. Photograph the installed format parts.
2. Challenge the full intended range: the largest and smallest product, each pocket geometry, minimum and maximum operating speeds, and at least one restart after a controlled stoppage. Inspect for trapped doses, chipped tablets, cracked coatings, split capsules, and distorted soft capsules.
3. Measure recovery and damage against pre-set limits. Reconcile loaded doses, recovered doses, rejects, trapped product, damaged units, and unexplained loss; a smooth-running de blistering machine can still hide incomplete extraction.
4. Use vision inspection to identify missing, broken, or visibly damaged units, but do not treat a clear image as proof of coating integrity, dose uniformity, or chemical quality. Define risk-based sampling, identity testing, assay, or other analytical tests before approving recovered product.
5. Simulate a jam or power interruption. Segregate accumulated blisters, partially processed packs, and product left in the feed path, then document line clearance and reconciliation before release or rework.
6. Approve the setup only when signed trial results, inspection records, test reports, cleaning checks, and the final settings sheet are complete. Preserve them as the repeatable changeover record.
How Maintenance, Cleaning and Safety Protect De-Blistering Results
A de blistering machine preserves recovery performance only when wear, residue and machine status remain controlled. Inspect punches, rollers, pocket supports, guides and discharge chutes at a defined interval; worn edges can crack tablets, leave product in cavities or create plastic and foil fragments.
Record lubrication, fastener checks, sensor tests and replacement parts in the equipment log.
Use a written cleaning and changeover checklist:
- Remove recovered product, empty blisters and waste before cleaning.
- Vacuum fines with suitable dust extraction; do not blow them across product-contact surfaces with compressed air.
- Inspect inaccessible pockets, chutes and guards under adequate lighting.
- Identify the new product, blister format, tooling and collection bins before restart.
- Reconcile material after a jam, power loss or partial batch, then segregate interrupted material until disposition.
- Apply lockout/tagout before reaching into the feed path, and verify guards, interlocks and emergency stops before operation.
Ask a pharmaceutical machines manufacturer to document cleaning access, dust-extraction performance, safe stoppage and restart, and format-specific line-clearance steps.
| Control | What to verify | Failure prevented |
|---|---|---|
| Preventive maintenance | Punch alignment, roller condition, sensors and fasteners | Breakage, incomplete extraction and unplanned stoppage |
| Dust control | Gentle separation plus extraction that does not pull capsules or tablets into waste | Fines, cross-contamination and exposure |
| Cleaning | Product-contact surfaces, hidden cavities and changeover inspection | Residue, contamination and mix-ups |
| Safety | Guards, interlocks, emergency stop and lockout points | Hand injury during jams or cleaning |
How to Choose Equipment and Decide Whether Recovery Is Worthwhile
Compare recovery cost per accepted dose, not machine speed. Include labour, sorting, cleaning, changeover, rejected product and downtime; mechanisation is worthwhile when it raises intact recovery and reduces handling without creating a larger testing or reconciliation burden.
| Option | Labour and control | Failure exposure | Best use |
|---|---|---|---|
| Manual opening | Low equipment cost, high operator time; inspect each dose by hand | Inconsistent force, contamination and counting errors | Small lots, unusual formats or temporary recovery |
| Mechanised recovery | Repeatable force and higher output; requires setup, cleaning and validation | Hidden damage after wrong format adjustment or interrupted runs | Recurring volumes with stable blister formats |
| Outsource recovery | No equipment purchase; pay for external capacity and oversight | Transport, chain-of-custody and release delays | Occasional campaigns without internal capability |
Give the supplier a performance envelope, not “packs per minute.” Specify supported PVC, PVDC, aluminium and foil structures; blister length, width and pocket pitch; tablet and capsule dimensions; minimum intact-dose recovery; maximum chipped, cracked or deformed units; residual foil or plastic limits; dust extraction; format changeover time; vision inspection; cleaning access; and records for qualification and preventive maintenance.
- Require adjustable punches or rollers, force settings and a repeatable setup record.
- Require format-specific guides, pocket supports, feed and reject settings, plus line-clearance instructions.
- Require controlled stop and restart, interrupted-material segregation, reconciliation and jam recovery.
- Ask for factory trials using your rejected packs, not sample cards alone.
A pharmaceutical machines manufacturer should provide test data that separates yield, intact units, rejects, contamination and downtime. A pharma machinery manufacturer should explain sampling and analytical testing beyond vision inspection. For Jicon Technologies Pvt Ltd, ask these questions before comparing its proposal with another pharmaceutical machinery manufacturer.
Frequently asked questions
How do you measure de-blistering machine performance?
Track recovery rate, damaged tablets or capsules, throughput, stoppages and rejected product across a defined trial batch.
How do blister materials and product shapes affect recovery?
PVC, PVDC-coated film, aluminium foil, tablet profiles and capsule sizes change the force and alignment needed for clean separation.
What should a de-blistering format trial include?
Test each blister format with representative products, record recovery and damage results, then approve recovered product through documented quality checks.
How do maintenance, cleaning and safety protect de-blistering results?
Inspect punches, rollers, guides and guards; clean product-contact parts between formats; and isolate energy before servicing.