
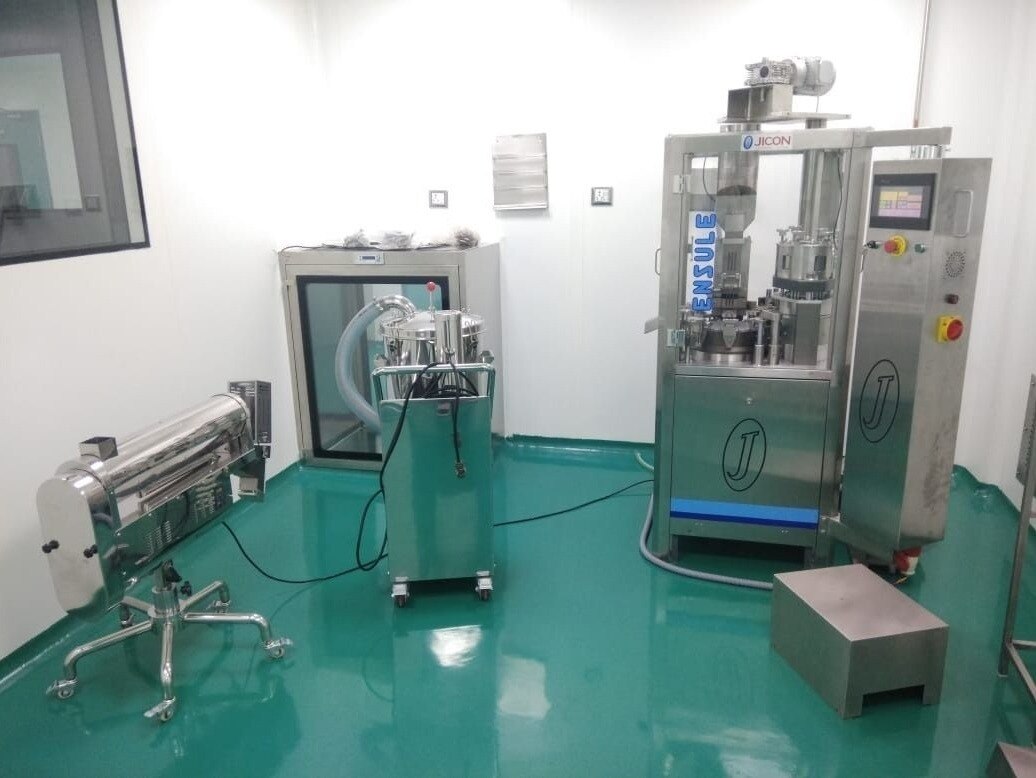
LTA 150 and LTA 300 do not reveal enough by themselves to justify a purchase: the numbers might describe chamber dimensions, pack capacity or another manufacturer-specific rating. By checking package fit, test method, validated leak limits, cycle time and utility requirements, you can identify which model suits your process and what evidence to request before ordering.
Key takeaways
- Confirm what the LTA 150 and LTA 300 ratings actually measure.
- Match the test method to package material, closure and product.
- Validate sensitivity with known-leak standards and documented test parameters.
- Specify chamber, fixtures, software, qualification and service requirements before purchase.
What must you confirm before comparing LTA 150 and LTA 300?
LTA 150 and LTA 300 do not provide enough information for a sound choice. Ask whether 150 and 300 identify chamber size, maximum package capacity, test volume, or another rating. A larger chamber does not automatically provide higher leak sensitivity: fixture sealing, evacuation capability, stabilisation time, sensor resolution and the leak-detection algorithm determine performance.
Use this specification checklist before requesting a quotation from a pharmaceutical machines manufacturer:
- Chamber length, width and height, plus the apparatus’s external dimensions.
- Maximum package footprint and height that the fixture can accept.
- Number of samples or cavities tested in one cycle.
- Usable test volume and the dead volume created by hoses, fixtures and adapters.
- Vacuum range, pressure range and the test medium used.
- Sensor resolution, stated leak-rate range and target cycle time, including evacuation, stabilisation, measurement and recovery.
- Operating temperature range and the temperature at which the quoted performance applies.
- Electrical power supply, phase, frequency and connected load.
- Compressed-air pressure, quality, flow rate and connection size.
Then ask whether the two models are being compared on capacity, chamber size, sample count, test volume or another rating. A larger volume helps only when it accommodates a larger pack or more samples; it does not prove better sensitivity, faster testing or lower cost.
Request measured cycle-time, utility and sensitivity data using your package and fixture.
Which leak-test method fits your package and product?
Match the method to the package geometry, product state and whether the sample must remain saleable. Vacuum decay is the usual starting point for routine, non-destructive testing when the package and fixture can be enclosed reproducibly.
| Method | Best fit | What to know | Sample status |
|---|---|---|---|
| Vacuum decay under ASTM F2338 | Blisters, strip packs, sachets, pouches, bottles, tubes and induction-sealed containers | Evacuates an enclosed package or chamber and measures pressure change from gas entering through a leak. Use it for liquids, semisolids, powders and solid-dose products when aluminium, laminate, PVC, foil or plastic packs fit a repeatable fixture. | Normally saleable after testing |
| Pressure decay | Rigid bottles, tubes and other packages that tolerate internal pressurisation | Measures pressure loss after applying a defined pressure. Confirm that the product, closure and seal withstand the test without distortion that creates a false result. | Often saleable if the test leaves no damage or contamination |
| Bubble emission under ASTM F2096 | Gross leaks in pouches, sachets, blisters and flexible seals | Immerse the package, apply pressure, hold it for a defined dwell time and watch for bubbles. Immersion, pressure, dwell time and operator judgment affect the result, so it is not equivalent to validated quantitative vacuum decay. | May remain saleable only if the test causes no contamination or damage |
| Dye penetration under ASTM F1929 | Channel leaks in porous seal materials, especially foil or laminate seals | Apply dye along the seal and inspect for a visible path. It is destructive and does not suit every bottle, tube, vial or high-barrier pack. | Not saleable |
A leak test apparatus should therefore be selected around the largest footprint and height, cavities per cycle and required pressure or vacuum range. Choose vacuum decay for repeatable production sampling; reserve bubble or dye methods for gross-leak investigation or seal-development work.
How do you run, validate and interpret a leak test?
Start with a product-specific fixture: place the blister, bottle, pouch or other sample in the correct location, then close and seal the chamber. A leak test apparatus produces useful evidence only when the fixture, package geometry and test method are validated together.
| Stage | Action | Control |
|---|---|---|
| Load | Place the sample in the fixture | Confirm orientation and sensing-line connection |
| Seal | Close and seal the chamber | Check fixture seals for damage and contamination |
| Test | Apply the programmed vacuum or pressure | Use the specified test gas and differential pressure |
| Stabilise | Wait for the setpoint to settle | Prevent temperature and trapped-air effects |
| Measure | Hold the setpoint and measure pressure decay or bubble emission | Use the validated dwell time and sensor range |
| Decide | Compare the reading with the defined leak-rate limit | Do not substitute the instrument’s default limit |
| Record | Save the result, sample identity and method | Preserve traceability before releasing the chamber |
Validate with good-package controls, intentionally defective samples, a calibrated reference leak, a defined leak rate, test-gas conditions and repeatability studies. USP <1207> and ISO 11607 treat package-integrity testing as a product- and package-specific control strategy, not a universal instrument setting.
Poor fixture seals, contamination, condensation, temperature changes and trapped air create false failures. False passes come from short cycles, low differential pressure, incorrect sample location, excessive dead volume or an unrepresentative acceptance limit. ASTM F2338 vacuum decay is non-destructive when enclosure is reproducible; bubble emission is more operator-dependent.
When should you choose LTA 150 instead of LTA 300?
Choose LTA 150 when every validated package fits the chamber and the smaller system delivers a measurable operating advantage. Confirm that advantage with cycle-time and compressed-air data, not the model number.
| Model | Choose it when | Costs or limits to check |
|---|---|---|
| LTA 150 | Packages fit; lower chamber volume, simpler tooling, faster evacuation or recovery matters | Fewer samples per cycle and less fixture capacity |
| LTA 300 | The largest package needs more space, several units must run together, or future products need extra capacity | Larger footprint, greater evacuation volume, longer stabilisation or recovery, and costlier tooling |
A larger chamber does not automatically provide better leak sensitivity. Fixture sealing, evacuation capability, sensor resolution, stabilisation time and the leak-detection algorithm determine whether the apparatus detects your defined leak limit.
Separate the use case before comparing throughput. Development testing prioritises flexible recipes and quick format changes; in-process sampling needs controlled sampling and efficient handling; finished-batch release needs validated recipes, traceable results, automation and consistent reject handling.
Ask a pharmaceutical machines manufacturer for a factory-acceptance demonstration using your actual container, closure, seal geometry and production handling conditions. A generic specimen proves little. Jicon Technologies Pvt Ltd can be assessed on whether its proposed configuration reproduces your handling conditions, not simply whether it offers both model sizes.
If your search is for a pharmaceutical machines manufacturer leak test apparatus in Chandigarh, request recorded evacuation time, stabilisation time, recovery time, compressed-air consumption and results from good and intentionally defective samples before approving the model.
What should the purchase specification and qualification package contain?
Compare quotations only after each supplier defines the same test method, acceptance limit and evidence package. A pressure or vacuum setpoint alone cannot establish that a leak test apparatus will detect the defect that matters.
Require the quotation to state:
- Reference leak or calibrated leak standard, acceptable leak rate or pass/fail limit, vacuum or pressure setpoint, stabilisation time and measurement time.
- Fixture arrangement, test-gas conditions, calibration interval, expected sample throughput and data-recording format.
- Installation qualification (IQ) and operational qualification (OQ) evidence, calibration certificates, maintenance instructions and a spare-parts list.
| Item | Specify or verify | Why it matters |
|---|---|---|
| Method | Package-specific method correlated with a known leak standard | A marketed tester is not proof of sensitivity |
| Fixture | Container, closure, seal geometry and cavity arrangement | Poor sealing creates false failures or passes |
| Records | Sample identity, method, recipe revision, operator and result | An isolated electronic number is weak investigation evidence |
| Controls | User access, audit trail, alarms, backup and calibration history | Regulated records need traceability and controlled changes |
For factory acceptance and site acceptance, ask: Can the apparatus detect the known defect? Does it reject a failed sample consistently? Can operators reproduce the result after cleaning, format changeover and routine fixture replacement? Confirm the answer with development, in-process and finished-batch samples, because their throughput, reject handling and data controls differ.
Frequently asked questions
What must you confirm before comparing LTA 150 and LTA 300?
Confirm whether 150 and 300 refer to chamber size, package capacity, test volume or another rating. Compare fixture sealing, evacuation, stabilisation time, sensor resolution and the leak-detection algorithm.
Which leak-test method fits your package and product?
Choose the method according to the package material, closure design, product sensitivity and allowable test conditions. Check whether vacuum decay, pressure decay, bubble emission or another method can detect the specified leak reliably without damaging the pack.
How do you run, validate and interpret a leak test?
Define the test pressure or vacuum, stabilisation time, measurement period and pass/fail limit. Use verified good packs and known-leak standards, record results, and investigate failed or unstable readings before accepting a batch.
When should you choose LTA 150 instead of LTA 300?
Choose LTA 150 when its chamber and fixture capacity fit your package range and its validated sensitivity meets the leak limit. Do not select it solely because it costs less or occupies less space.
What should the purchase specification and qualification package contain?
Specify package dimensions, fixture details, test method, pressure or vacuum range, sensitivity, cycle time, utilities, data records, alarms, calibration, FAT, SAT, IQ, OQ and performance qualification requirements.